A spray nozzle never fails suddenly. It fails on a schedule that was written the day it was installed — by the abrasive content of the liquid, the pressure behind it, and the material in the orifice. Most plants never read that schedule; they notice the nozzle when the coating is already patchy or the cooling zone has shifted. This page walks through the life of one nozzle stage by stage, what changes at each stage, and the readings that let you see the drift coming. The nozzle family itself is on the CRAC ceramic nozzles page.
Day One: Write Down the Baseline
Everything later depends on numbers nobody took at the start. On commissioning day, record three things: the flow rate at working pressure, the spray angle across the width, and a photograph of the spray pattern on a dry surface. Ten minutes of measuring becomes the reference that every future check is compared against. It is also the moment to confirm the orifice is clean and the seal is seated — a surprising share of "wear" complaints trace back to damage inflicted during installation, not to service.
The First Weeks: Nothing You Can See
Early wear is invisible from the floor and measurable in the log. Slurry flowing through the orifice removes material from the inlet edge a few microns at a time; flow creeps up by a percent or two, the spray angle widens by a degree, and none of it is perceptible without the baseline. This is the stage where a monthly five-minute check — flow at pressure, angle, pattern photo — pays for itself, because it catches the drift while the process still compensates for it automatically.
The Middle of Life: The Drift Becomes Visible
By the time orifice enlargement reaches a few percent, the effects leave the log and enter the process. A wider opening passes more liquid at the same pressure, so pump load or flow total rises. The spray fan grows and its edges soften — coverage that used to end crisply now fades, and adjacent sprays begin to overlap or, at the deck edges, to miss. Droplets get coarser as the jet loses energy, which in cooling or coating duty shows up as wetter patches and slower evaporation. In abrasive slurry duty the same physics runs in reverse: the jet erodes whatever it lands on faster, because the stream is wider and less coherent.
Late Life: Quality Loss, Not Just Spray Loss
The final stage is where deferred replacement starts to cost product. Coarse, drifting sprays produce uneven coating thickness, off-spec drying zones, or — in classification and grinding circuits — spray water landing where it was never aimed, attacking liners and bearings. A steel nozzle at this age also begins to shed its own material into the stream. The rule of thumb worth adopting: when the measured flow has drifted five percent from baseline, or the pattern photo shows a visibly asymmetrical fan, the nozzle's process value is already spent even if it still sprays.
The Same Life, Slower: Why Material Moves the Dates
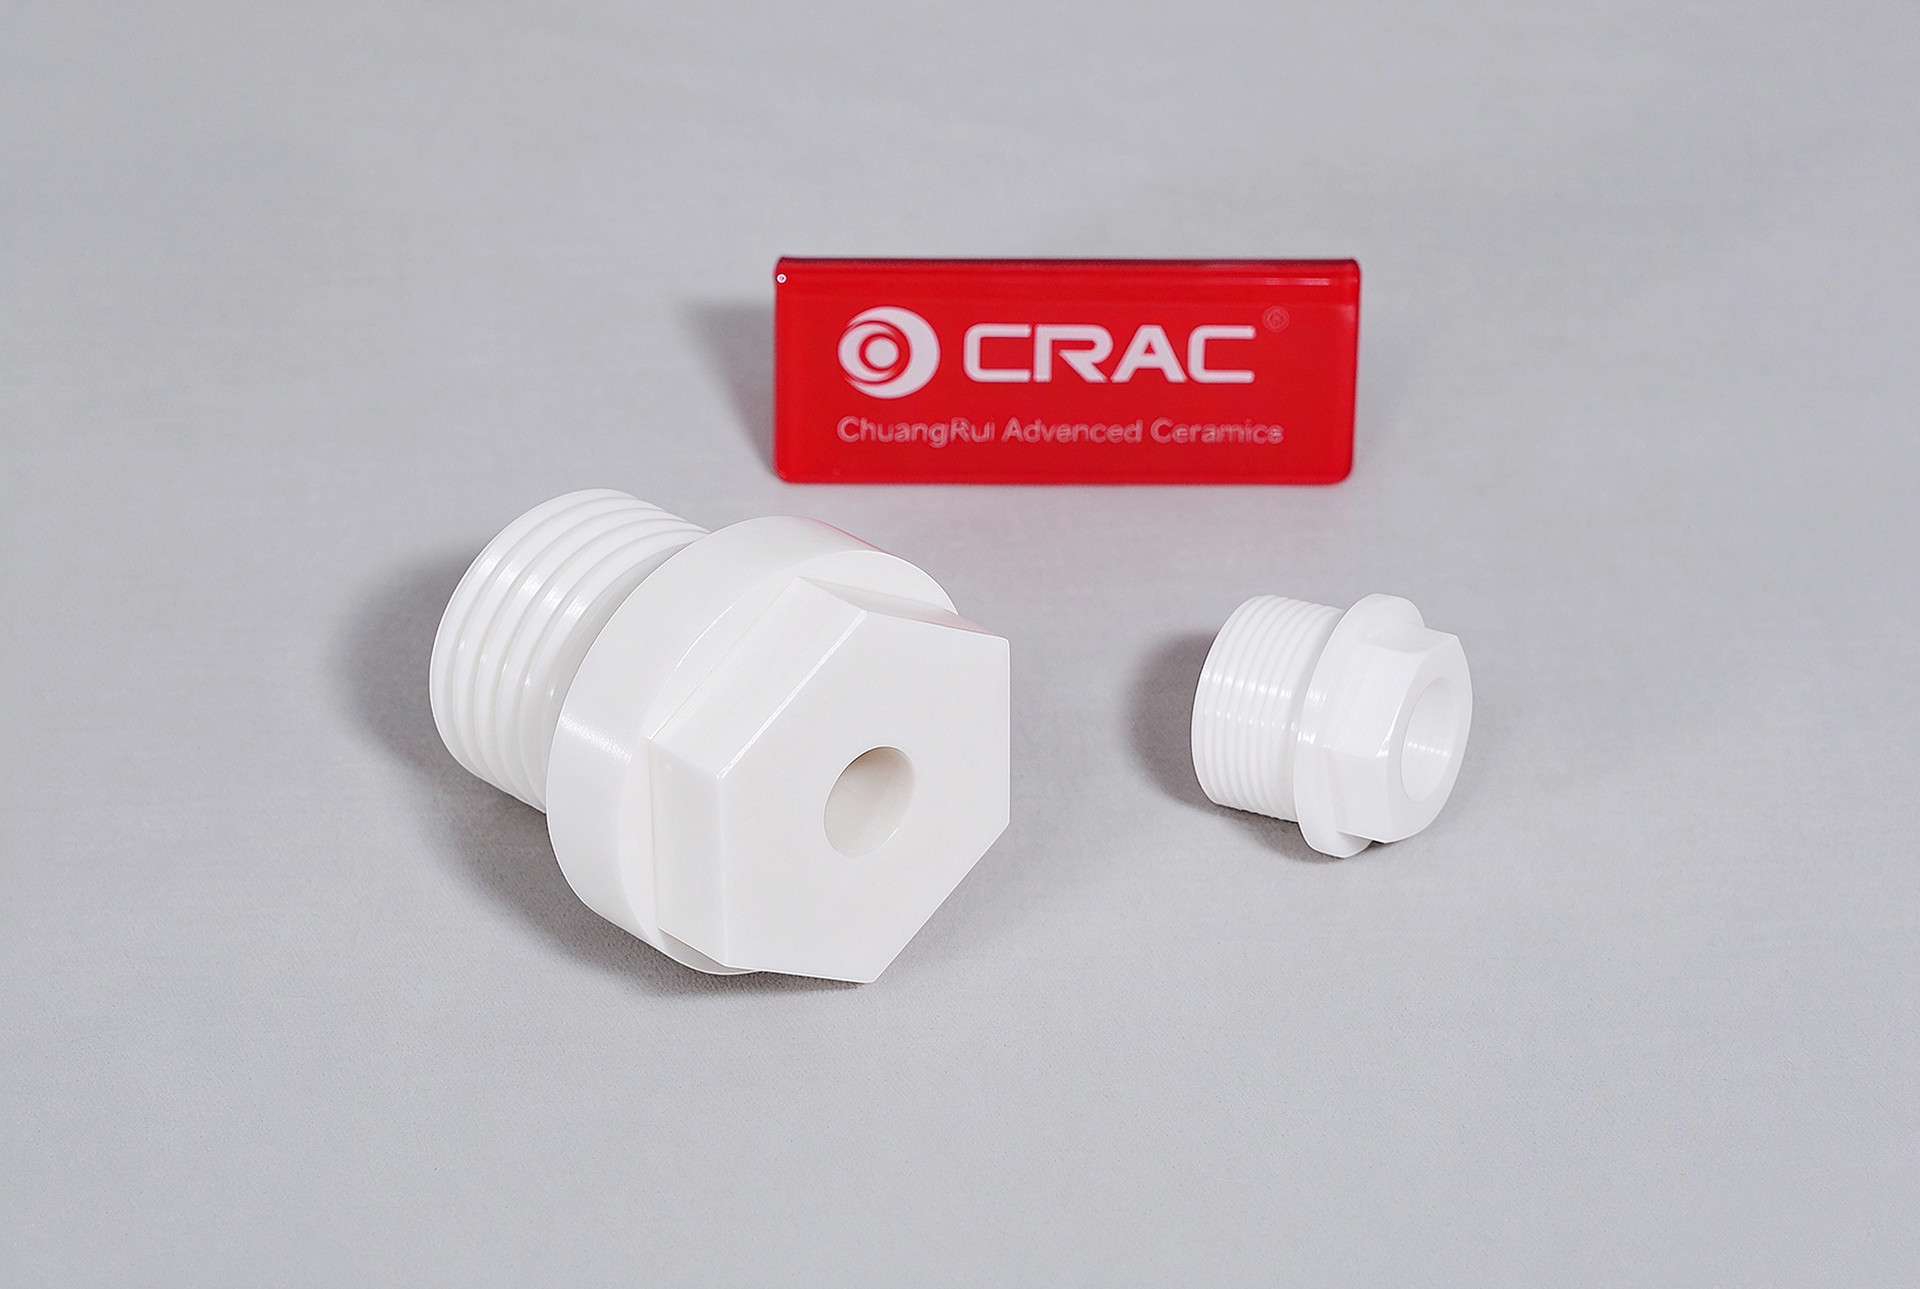
Nothing in the timeline above changes with nozzle material — only the dates do. The orifice of a zirconia nozzle resists abrasive enlargement by an order of magnitude better than hardened steel, so every stage of the drift stretches out and the replacement interval extends from weeks to months. That is the entire argument, and it is why the choice between steel, alumina and zirconia is really a choice about how often you want to climb up to the spray deck. The grades are compared in the material classification guide and the zirconia selection guide; for the harshest duties, see zirconia parts for extreme wear.
Making the Timeline Longer
Three practices reliably stretch any nozzle's life, whatever it is made of:
- Filter upstream. Most orifice damage is a single oversized particle, not gradual erosion. A strainer sized to the nozzle is the cheapest life extender there is.
- Discipline the pressure. Running above design pressure raises wear disproportionately — erosion scales steeply with velocity, so a modest overspeed costs much more than a modest gain.
- Handle ceramics like ceramics. The one way to fail a zirconia nozzle early is a steel tool against the orifice during fitting. Torque the seals, not the nozzle body.
For plants that spray abrasive slurries continuously — mills, classifiers, scrubbers — the nozzle usually wears alongside the rest of the wetted circuit; pairing it with bead-mill ceramic parts or ceramic dispersion discs keeps replacement windows aligned instead of staggered.
Questions From the Spray Deck
Can we detect orifice wear without shutting down?
Often, yes: a rise in total flow at constant pressure across a bank of nozzles is the aggregate signature. Localize the worn unit by segmenting the bank or inspecting the pattern photos monthly.
Is a wider spray angle always a sign of wear?
Usually, but not only — a partly blocked outlet can also distort the fan. Asymmetry points at blockage or damage; uniform widening points at wear.
Do ceramic nozzles fit our existing holders?
Standard thread and flange forms are routinely matched; custom bodies are made net-shape by ceramic injection molding (with the precision route for volume programs), so a retrofit rarely needs new hardware. The OEM/ODM program works from your drawing, and zirconia structural parts covers the wider engineering context.
We spray above 100 bar. Is ceramic still the answer?
High pressure is exactly where ceramic pays most — wear scales steeply with velocity, so the gap between steel and zirconia life widens with every bar. Say the word and we will size the orifice for the duty.
Send us the pressure, the slurry and the pattern — we will size a nozzle that lasts.